Top Benefits of Installing a Monorail Wire Rope Hoist in Ahmedabad Industries
Introduction
Modern industries require reliable material handling equipment to improve productivity, maintain workplace safety, and reduce manual effort. A Monorail Wire Rope Hoist is an efficient lifting solution designed to move heavy materials along a fixed overhead track. It is widely suitable for manufacturing plants, engineering workshops, warehouses, fabrication units, and industrial production facilities where repetitive lifting and transportation operations are essential.
Ahmedabad is a major industrial hub in Gujarat, with businesses operating in engineering, pharmaceuticals, chemicals, textiles, automotive components, and machinery manufacturing. These industries often need dependable lifting systems to handle raw materials, finished products, equipment, and heavy components. Installing a suitable monorail hoist can help streamline these operations while making better use of available floor space.
Stalmac Cranes provides industrial crane and material handling solutions for businesses seeking efficient lifting arrangements. Choosing a properly specified Monorail Wire Rope Hoist Manufacturer in Ahmedabad can help industries select equipment according to their lifting capacity, operating environment, travel requirements, and production needs.
What Is a Monorail Wire Rope Hoist?
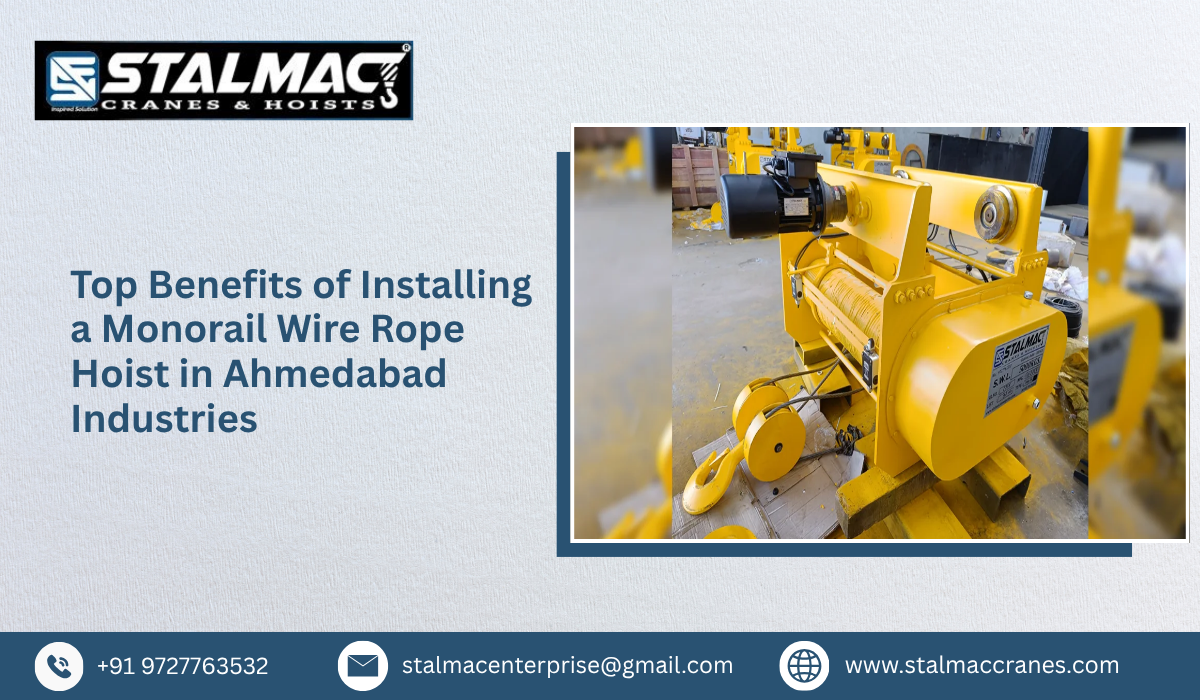
A monorail wire rope hoist is a mechanical or electrically powered lifting device that uses a wire rope, hoisting drum, motor, braking arrangement, and associated controls to lift and lower loads. The hoist generally travels along a single overhead rail or beam, depending on the system configuration.
An Electric Monorail Wire Rope Hoist combines powered lifting with controlled horizontal movement along the monorail track. This arrangement allows operators to transfer materials between designated workstations without requiring extensive floor-level transportation equipment.
Industries can select a Heavy Duty Monorail Wire Rope Hoist for demanding applications involving frequent lifting cycles or substantial loads, provided the equipment is engineered for the required duty classification and operating conditions.
Top Benefits of Installing a Monorail Wire Rope Hoist in Ahmedabad Industries
1. Improved Material Handling Efficiency
A monorail hoist helps move materials between workstations through a defined overhead route. This reduces dependence on manual handling and can improve the consistency of production workflows.
Businesses working with machinery parts, metal assemblies, industrial components, and packaged materials can benefit from controlled lifting and transportation. A well-planned system also helps reduce unnecessary material movement and improve operational coordination.
2. Better Utilisation of Available Floor Space
Industrial facilities often need to accommodate machinery, storage racks, assembly lines, and employee movement within limited floor areas. Overhead material handling helps keep much of the floor clear by moving loads above the working zone.
For Ahmedabad factories with space constraints, a monorail system can support more organised material movement without requiring a large floor-mounted transportation arrangement.
3. Enhanced Workplace Safety
Handling heavy loads manually can expose workers to strain, dropped materials, and other operational hazards. A properly designed hoist provides controlled lifting and lowering, helping reduce the need for direct manual handling.
Important safety features may include overload protection, limit switches, emergency stop controls, and reliable braking systems, depending on the equipment specification. Safe operation also requires trained operators, regular inspections, suitable load securing, and compliance with applicable safety requirements.
4. Consistent Lifting Performance
An appropriately selected Monorail Wire Rope Hoist Manufacturers in India offering should be evaluated on lifting capacity, lifting speed, operating duty, and expected service conditions. Wire rope hoists are useful where stable lifting performance and controlled load positioning are important.
With suitable maintenance and correct operation, these systems can support repetitive industrial lifting requirements and help minimise avoidable interruptions.
5. Adaptability to Industrial Requirements
Different industries have different lifting heights, load dimensions, movement routes, and production layouts. A monorail hoist can be specified for a particular beam arrangement and travel distance, subject to structural and engineering assessments.
Working with experienced Monorail Wire Rope Hoist Suppliers in India helps businesses evaluate available configurations and identify equipment suited to their operational requirements.
Key Advantages of a Monorail Wire Rope Hoist
The following advantages make monorail hoists a practical option for many industrial applications:
- Reduced manual effort: Mechanised lifting supports the handling of heavy components and materials.
- Space optimisation: Overhead movement helps preserve valuable floor space.
- Controlled load movement: Powered lifting and travel options can improve handling consistency.
- Workflow efficiency: Fixed routes support predictable movement between designated workstations.
- Flexible configuration: Systems can be selected according to lifting height, rated capacity, and track layout.
- Operational reliability: Correct equipment selection, inspection, and maintenance support dependable performance.
- Integration potential: A suitable hoist may be incorporated into existing production or material handling arrangements after engineering evaluation.
These benefits depend on proper installation, equipment suitability, operator training, and preventive maintenance.
Industrial Applications of Monorail Wire Rope Hoists
A Monorail Wire Rope Hoist can support a variety of material handling activities across Ahmedabad's industrial sectors.
- Engineering and Manufacturing: Lifting machine components, fabricated assemblies, and production materials.
- Automotive Industries: Moving vehicle components, heavy assemblies, and tooling between workstations.
- Textile Industries: Handling selected machinery components and maintenance equipment.
- Pharmaceutical and Chemical Plants: Transferring compatible equipment and materials in designated handling areas, subject to site-specific safety requirements.
- Warehouses and Distribution Centres: Moving heavy goods along predefined overhead routes.
- Fabrication Workshops: Positioning metal sections, frames, and welded structures during assembly.
- Power and Industrial Maintenance: Lifting motors, pumps, and other serviceable equipment where the installed system is appropriately rated.
Before installation, businesses should assess load characteristics, operating frequency, environmental conditions, available headroom, and the complete travel path.
How to Choose the Right Monorail Wire Rope Hoist
Selecting the right hoist requires more than comparing lifting capacities or purchase prices. Industries should evaluate the following technical factors:
- Rated lifting capacity: Determine the maximum intended load, including any relevant lifting accessories.
- Lifting height: Confirm the vertical distance required to raise and lower materials.
- Travel distance: Measure the monorail route and identify the required movement between workstations.
- Duty classification: Match the hoist to the expected frequency, load spectrum, and operating cycles.
- Lifting and travel speeds: Select suitable speeds for production requirements and load control.
- Safety provisions: Review braking, limit switches, overload protection, and emergency controls where applicable.
- Structural compatibility: Verify beam strength, supporting structures, wheel loads, and installation clearances through qualified engineering assessment.
- Maintenance support: Consider spare parts availability, inspection requirements, and service arrangements.
Businesses comparing the Best Monorail Wire Rope Hoist Manufacturer should examine technical specifications, manufacturing quality, documentation, warranty terms, and after-sales support rather than relying on price alone.
Why Consider Stalmac Cranes for Industrial Lifting Solutions?
Stalmac Cranes is a relevant point of contact for businesses exploring crane and industrial lifting requirements. When evaluating a project, buyers should discuss the intended application, rated capacity, lifting height, monorail travel, operating duty, and site conditions to determine the appropriate equipment configuration.
An experienced Industrial Monorail Hoist Manufacturer should be able to clarify technical requirements and help assess whether a standard or application-specific arrangement is appropriate. Buyers seeking a Monorail Wire Rope Hoist Supplier in Ahmedabad can also compare installation requirements, documentation, maintenance provisions, and service support before finalising their decision.
For projects involving interstate supply or overseas delivery, businesses may also evaluate the technical and commercial capabilities of Monorail Wire Rope Hoist Exporter in India companies. Confirming applicable standards, packaging, documentation, and destination-specific requirements is essential when planning procurement.
Conclusion
Installing a Monorail Wire Rope Hoist can help Ahmedabad industries improve material handling efficiency, utilise overhead space, reduce manual lifting, and establish more organised production workflows. Its suitability depends on the load, travel route, operating duty, structural arrangement, and safety requirements of the facility.
Whether a business needs an Electric Monorail Wire Rope Hoist for routine production or a Heavy Duty Monorail Wire Rope Hoist for demanding industrial operations, careful technical evaluation is essential. Stalmac Cranes can be approached to discuss project requirements and identify suitable industrial lifting solutions.
Contact Stalmac Cranes through stalmaccranes.com to discuss your material handling needs and explore a monorail hoist configuration suited to your facility.

